How to Match a Hydraulic Hammer to Your Excavator
Match a hydraulic hammer to your excavator on three numbers: the carrier's operating weight range, the hydraulic oil flow available on the breaker line, and the working pressure the carrier can hold. If any of the three sits outside the hammer maker's stated window, the combination will either underperform or destroy itself, and most hammer problems blamed on build quality are actually carrier mismatches.
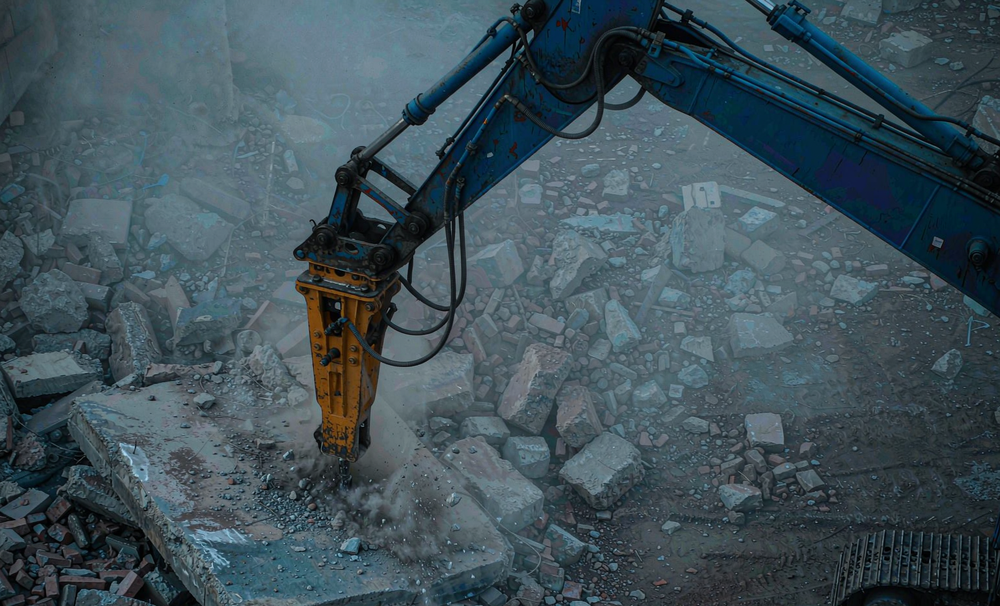
What does the carrier-weight window actually protect?
Every hammer model carries a carrier weight range, for example 11 to 16 tonnes. That range is not marketing padding; it reflects the boom geometry, stick strength and counterweight of machines the bracket and mounting pins were designed for. Hang a hammer on a machine below the window and the carrier gets kicked around by every piston stroke, which fatigues the boom welds and beats the front head pins to death. On a machine above the window, the hammer is simply underpowered for the rock the machine can reach, and the extra boom mass loads a bracket sized for lighter sticks.
What happens when oil flow is wrong?
The breaker piston is driven by oil flow, so flow controls impact rate. Underflow a hammer and the stroke slows, cycles get long, and the energy that does arrive turns into heat instead of rock-breaking; carrier oil temperatures climb into the warning zone on hot days. Overflow it and the piston overspeeds, which spikes operating pressure, hammers the tool and bushings, and is the fastest known way to crack a chisel. A hammer sold for a 13 tonne carrier typically draws somewhere in the 90 to 140 litres per minute class at 150 to 180 bar, but this varies by model and brand, so read the specific flow-pressure chart rather than assuming from tonnage alone.
Pressure matters just as much. The carrier's relief valve setting must reach the hammer's stated working pressure or the piston never completes its power stroke, and it should not exceed the hammer's maximum or the accumulator and seals carry the difference.
Why does the mounting bracket matter as much as the hammer?
The bracket connects the hammer to your stick, and stick cross-sections vary between brands of the same tonnage. A mismatched bracket face lets the hammer rock on its mount, which concentrates load on the mounting pins and through bolts instead of the tool. Through bolts in particular are consumables on a working breaker, and they should be checked for tightness daily in the first week after fitting, because a loose through bolt hammering in its pocket quickly becomes an elongated bolt hole. When replacing them, use parts made for the hammer model rather than close-enough hardware — for example through bolts and spare parts for a Furukawa HB 15G class hammer rather than an unlabelled bolt of similar size.
What should you check before the first operation?
- Confirm the carrier's breaker-line flow and relief setting against the hammer chart, with the engine at the RPM the chart specifies.
- Check nitrogen precharge in the backhead at the stated pressure before start-up and again after the first shift, because transport and new seals both leak a little.
- Confirm the carrier's oil cleanliness and cooler capacity; a breaker is less forgiving of dirty oil than a bucket cylinder, and overheated oil voids more warranties than any other single cause.
- Plan the first hour on soft material. Blanking the hammer in air, an unloaded stroke with no rock under the tool, bends the tool and shocks the mount; operators should stop the stroke the moment the rock breaks.
Which tool point suits the job?
Moil points concentrate energy for hard, monolithic rock; chisel tools suit trenching and layered material; blunt tools are for secondary breaking of already-fractured rock. The right point cuts cycle time as much as the flow match does, and a worn point does the opposite. Tools, through bolts and mounting pins are all wear items you will buy repeatedly — breaker tools and drill rods as well as hammer pins are worth pricing before you commit to a hammer, because the availability of its consumables matters more than the spec sheet.
How do you spot a mismatch early, before it costs a hammer?
Three symptoms point straight at carrier matching. First, impact rate that drops after ten or fifteen minutes of work while carrier oil temperature climbs: the machine cannot hold the hammer's flow demand, so either the pump is worn or the hammer is oversized for the line. Second, impact rate that is too fast and sounds sharp: the piston is overspeeding on excess flow, and the tool will show shiny, polished scuffing at the bushing contact band long before it cracks. Third, a hammer that rocks visibly in the bracket at every stroke: the mounting pin clearance has opened up, usually because a mismatched bracket let the load concentrate from day one. Any one of these is cheaper to correct in the first week than in the third month, when the front head bushing and the tool both need replacing.
None of these checks need special instruments. A stopwatch on the impact rate, an infrared thermometer on the return line, and a weekly look at the through bolts will catch nearly every mismatch while it is still a settings problem instead of a parts problem.
,000 went viral in Norway this autumn, and behind that video sits hard data: construction machinery exports reached US.373 billion in the first half of 2026, up 21.7 percent year on year according to the China Construction Machinery Association, with compact equipment and micro excavators driving the fastest growth.
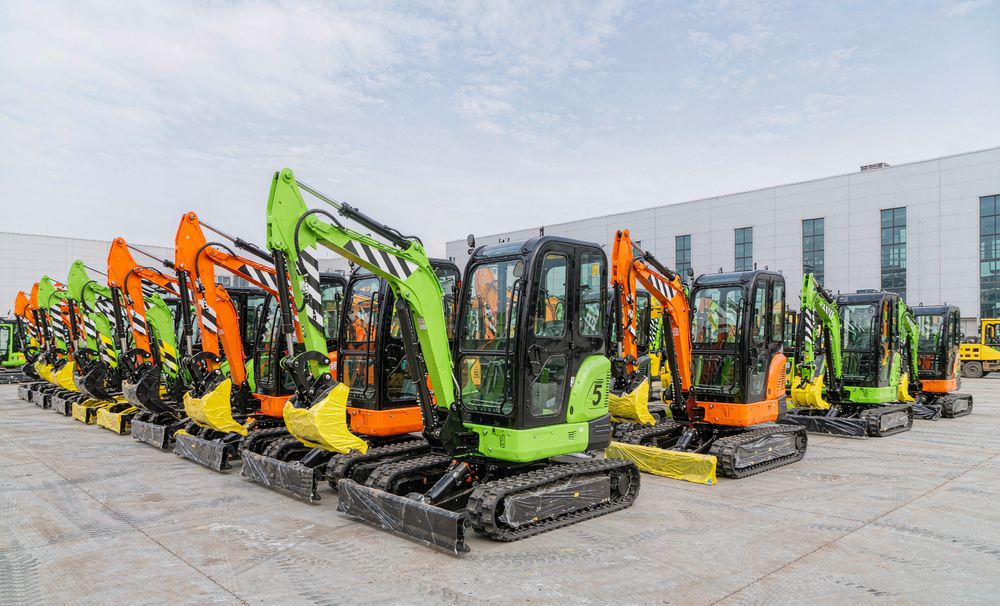
What do the H1 2026 export numbers show?
The headline figures reported by Chinese state media in late October, drawn from industry association statistics: excavator exports exceeded domestic sales for the eighth consecutive month, and cumulative excavator exports passed 85,000 units in the first seven months of 2026, up more than 31 percent year on year. Exports to the European Union reached US.626 billion, up 28.9 percent. Industry forecasts put China's compact construction machinery sales for 2026 above 180,000 units, with micro excavators making up more than 60 percent of that, roughly 110,000 machines. Trade commentary attributes the shift to buyers outside the traditional channel: private owners, small farms and tradespeople in Europe and South America discovering these machines through social media and cross-border e-commerce rather than dealer networks.
Why does this matter to parts buyers?
Because every one of those machines is a compact wear-parts consumer. A 1 to 3 tonne excavator still runs bucket pins and bushings, teeth, track rollers and sprockets; it just runs them at smaller envelopes and tighter tolerances than a 20 tonne machine. The parts market for this segment behaves differently from the large-machine market in three ways:
- Volumes are high and per-unit margins are thin, so parts supply consolidates around the same Shandong manufacturing clusters that build the machines.
- Many compact machines are sold direct to first-time owners, so sourcing spare parts is often the owner's first experience with the brand. A parts page that does not answer "which pin fits my machine" loses that buyer instantly.
- Fleet-scale after-sales networks, the normal channel for 20 tonne iron, barely exist for micro machines, which pushes owners toward online parts suppliers and pushes suppliers toward clear part-number discipline.
What does this mean for a Shandong parts maker?
JALE Excavator Parts is a Shandong manufacturer of excavator wear parts, and it sits inside the same industrial cluster that is shipping these machines. Unlike most parts suppliers, it also builds its own compact range, including the JALE08 and JALE12 mini excavators, so the fit between a small machine and its pins, bushings and undercarriage parts is designed rather than reverse-engineered.
Do compact machines need different parts discipline?
The wear parts are the same families, but the failure pattern is not. A micro excavator's pins and bushings are physically smaller, so a few tenths of a millimetre of wear is a larger share of the original clearance, and the symptoms, play at the bucket ear, grease that will not hold, a knocking sound on direction change, arrive sooner relative to machine hours. Owners who would never inspect a 20 tonne machine weekly can and should walk around a 1 tonne machine weekly: two grease strokes per pin, a visual check that the bucket ears have not bell-mouthed, and a feel for slop at the linkage. The parts themselves are cheap; the deciding factor is knowing the pin diameter and ear spacing before ordering, because a 25 mm and a 30 mm pin look identical in a photo.
One honest caveat: no association figures have been published for compact-segment parts demand specifically, so any claim about its size would be guesswork. What the export data does establish is the installed base: over 100,000 micro and compact machines a year are entering service, largely with owners who have no dealer relationship. Their pins, bushings and teeth will be replaced on wear, on the owner's budget, from whichever supplier answers first with the right dimensions. That is the market segment forming behind the headline number, and it buys the same discipline this site has always sold: correct part numbers, honest steel grades, and hardware that fits the first time.
.31 billion, up 47%, and to Latin America at US.03 billion, up 60.7%. Longer routes make schedule reliability worth more than a few days of inland saving, which is why the port and the carrier matter more than the canal itself.
What it means for a parts order in practice
Production time does not move. Machining, heat treatment and packing run at the same pace whichever port the container leaves from. What a shorter inland leg changes is the buffer a supplier needs between finishing an order and handing it to the carrier, and at the margin how much working capital sits in a container on a truck.
For the buyer, the response is unchanged: plan stock against ocean transit plus clearance, not against the inland leg, and ask for the port and the sailing date rather than a single lead-time number. The parts themselves — bucket pins and bushings, track chains, bucket teeth — are priced by steel grade and machining hours, not by which river they floated down.
.90 billion, up 13.9%; to Europe, US.59 billion, up 4.2%. The growth is elsewhere: Africa at US.31 billion, up 47%, and Latin America at US.03 billion, up 60.7%.
That regional split matters for spare-parts planning. Mature markets in Europe are growing slowly, while the fastest-growing destinations are markets where machines work long hours in abrasive conditions and where the dealer and service network is thinner — exactly the profile that generates high wear-parts consumption. Trade-press analysis attributes a large share of African excavator demand to mining, and mining duty is brutal on undercarriage and on ground-engaging tools.
What should buyers and distributors plan for?
Stock the models that are actually in the field, not the models in the press release. On the evidence of the last few years that means the mainstream 20–30 tonne classes and the household names built around them — PC200 and PC300 class machines, the 320 and 330 class, the EX200 class, the R210 class and the DX225 class — plus the undercarriage groups that fit them. Those are the machines absorbing pins, bushings and track components in volume.
Do not build stock around electric-specific parts yet. At 0.6% penetration there is no volume aftermarket, and the common parts on those machines are the same parts you already carry.
Finally, plan for the replacement cycle, not just the new-machine market. Chinese trade-press analysis puts the domestic replacement cycle at roughly eight years, and with domestic sales now rising on the back of equipment replacement and emission-standard upgrades, a large second and third-owner population of machines is coming into its maintenance-heavy phase. That is the cohort that buys the most wear parts per machine — and it is a diesel cohort.
